- 2B / BW Shalimar Bagh, Opp. BQ Market, Near DLF Mall New Delhi - 110088, India.
- :+91-9312-871-070
Manufacturers, Exporters, Suppliers of High Performance Powder Antiscalant
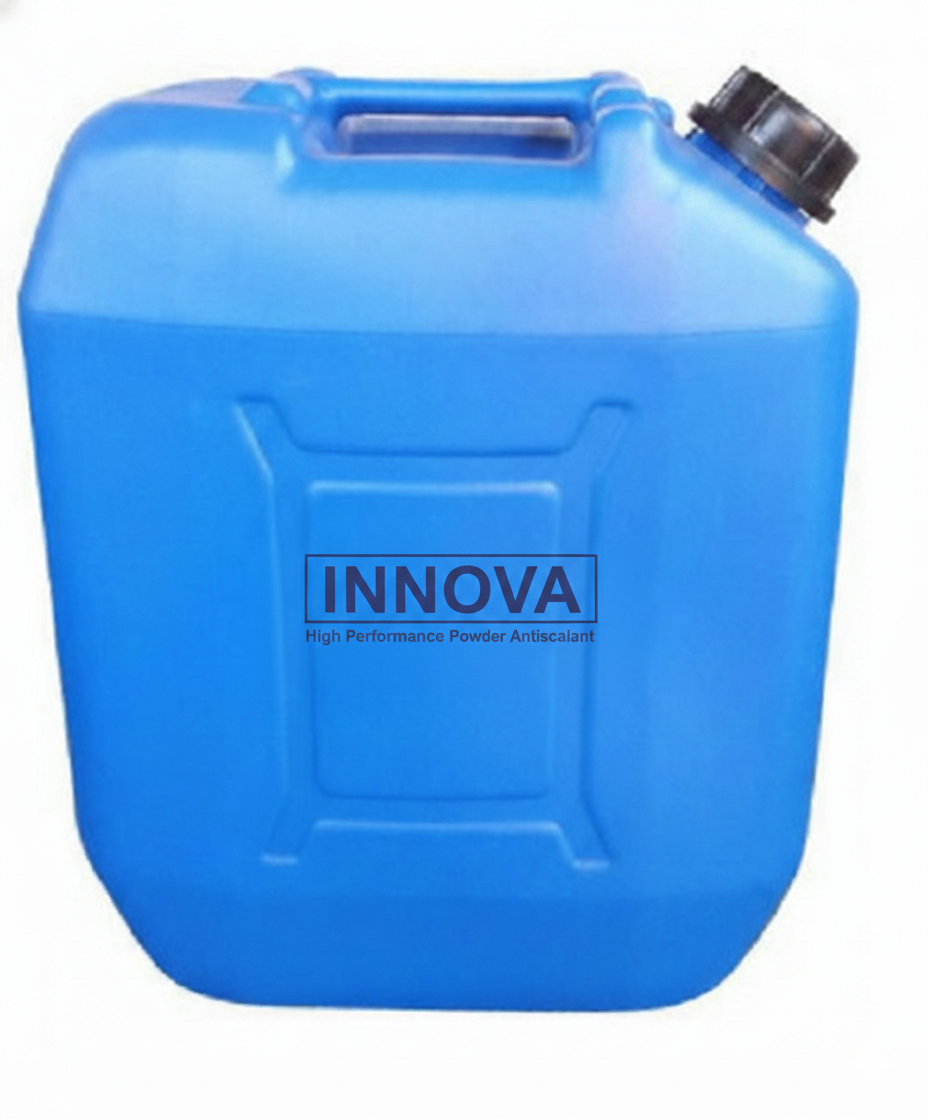
High Performance Powder Antiscalant in India (RO Membrane Treatment)
Innova Corporate (India) is a leading manufacturer, supplier and exporter of high-grade High Performance Powder Antiscalant in India. We offer the finest quality membrane treatment solutions at highly competitive prices for local industries. Our chemical formulations are engineered using pure raw materials, meeting global industrial quality standards to ensure maximum protection for your RO systems in India.
Our specialized Antiscalant/Antifoulant powder is designed for high-capacity membrane systems operating in India. It features a precise molecular weight range and a clear, impurity-free composition. This advanced formula effectively controls the scaling of carbonates and sulfate salts (Calcium, Magnesium, Barium and Strontium), while also preventing iron fouling and colloidal deposits common in India water sources.
Our powder formula is engineered for rapid solubility and is compatible with all major membrane types used in India plants. It is particularly effective in large-scale industrial units where storage space and logistics efficiency are priorities. By maintaining consistent flow rates and salt rejection, it helps in achieving the lowest possible operational cost per liter of treated water in India.
The powder format is especially advantageous for plants operating in remote or hard-to-reach locations, where liquid chemical transport is expensive and logistically challenging. A single 25 kg drum of our powder antiscalant is equivalent to multiple drums of liquid product, drastically reducing freight costs and warehouse space requirements. This makes it an ideal choice for India's growing base of decentralized industrial RO installations.
When dissolved as per recommended guidelines, the resulting solution is completely clear with no suspended particles or undissolved residue. This ensures clean, blockage-free dosing lines and prevents any risk of membrane surface deposition from the antiscalant itself. Plants in India that have switched from liquid to powder formulations consistently report improved membrane cleanliness and longer intervals between CIP cycles.
Strategic Advantages for India Industries:
- Highly Concentrated: Lower dosage requirements compared to standard liquid antiscalants, reducing overall chemical consumption and cost per cubic meter of treated water.
- Broad Spectrum Control: Effectively manages calcium carbonate, sulfate, and silica scales in India.
- Logistic Efficiency: Easy to transport and store with a longer shelf life in powder form.
- Membrane Safety: Fully compatible with Polyamide and Cellulose Acetate membranes.
- Cost-Effective: Reduces shipping costs to India and minimizes chemical handling hazards.
- Rapid Dissolution: Dissolves quickly in water for immediate dosing application.
- Extended Shelf Life: Remains stable for up to 24 months when stored in original packaging, unlike liquid antiscalants that degrade over time.
- Reduced Handling Risk: No risk of liquid spills, leaks or drum corrosion during storage and transport.
Recommended Applications in India:
- Large-Scale Industrial RO Plants across India where logistics and storage efficiency matter.
- Remote & Off-Grid Installations in areas with limited access to liquid chemical supply chains.
- High-TDS Borewell Water Treatment in hard-water regions of the country.
- Silica-Rich Water Sources where standard liquid antiscalants struggle to perform.
- Seasonal Operations where chemicals need to be stored for extended periods between use.
- Export-Oriented Units requiring consistent, high-purity chemical inputs.
Why Powder Antiscalant is Preferred Over Liquid in India:
- Lower Freight Cost: A fraction of the weight and volume compared to liquid, significantly reducing transport expenses across India.
- No Freezing Issues: Unlike liquid antiscalants, powder formulations are unaffected by low temperatures during winter transport in northern India.
- No Spillage Risk: Dry powder is far easier and safer to handle than corrosive liquid chemicals.
- Higher Active Content: Nearly 100% active ingredient vs. 30-50% in typical liquid formulations.
- Simplified Inventory: Fewer drums to track, stack and manage in your chemical store.
- Longer Shelf Life: Up to 24 months without loss of potency, ideal for strategic stockpiling.
Storage & Handling: To preserve the potency of the powder for your India facility, store in a cool, dry place within its original moisture-proof packaging. Always refer to the Material Safety Data Sheet (MSDS) for safe handling instructions and the Technical Data Sheet (TDS) for precise dilution and dosing ratios.